How to Reduce Changeover Time on an Automatic Rigid Box Making Machine
Reduce rigid box machine changeover time by staging materials and tools, following a standard setup sequence, and saving settings for repeat jobs.
What Is Changeover Time in Rigid Box Production?
Changeover time runs from the last acceptable piece of the previous job to the first approved piece of the next job. It includes adjustments, trial pieces and first-piece inspection. If the machine makes flat wrapped cases, measure at the case output rather than at finished box assembly.
What Should You Prepare Before a Machine Changeover?
While the current job is running, prepare the items you can stage away from the machine. This reduces time spent looking for materials, tools or instructions after the line stops.
- Materials: Stage the next job’s cover paper and grayboard. Check the paper orientation, board dimensions and panel layout against the job specification.
- Tools and parts: Gather any gauges, guides or change parts required for the next setup.
- Job references: Have the setup sheet, current drawing and approved sample ready for comparison.
Which Machine Adjustments Can Speed Up Changeovers?
A standard sequence helps operators avoid adjusting the same station twice. For example, set the paper feed and board guides first, verify board placement on the cover paper, then check folding and corner finish on a trial piece. Follow the sequence specified for your machine.
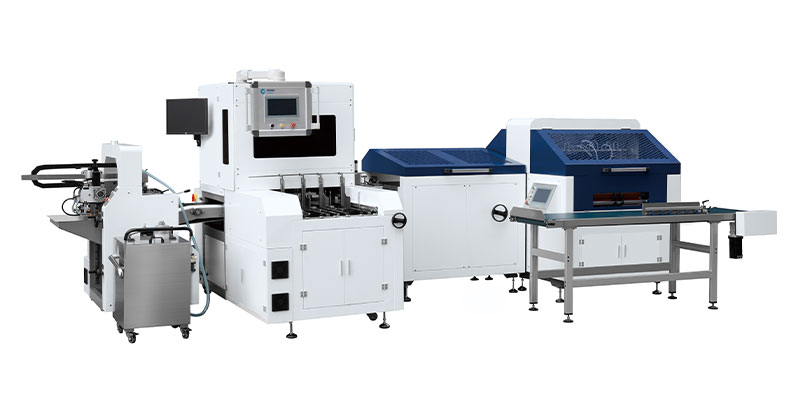
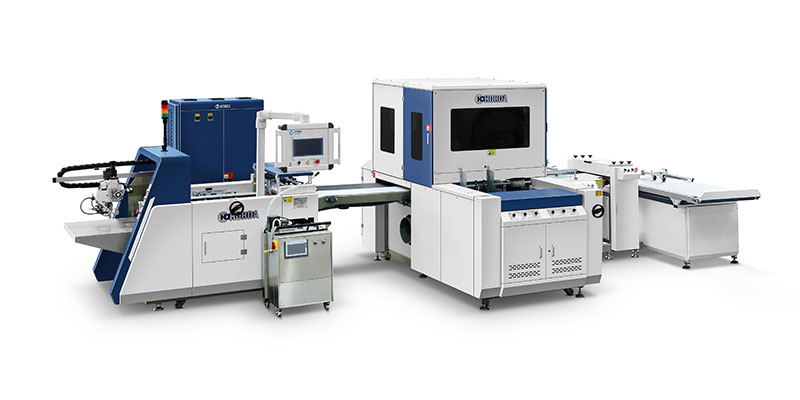
When comparing automatic rigid box making machines, check which settings are stored in the controller and which require manual adjustment. A saved program can recall supported settings, but guides, tooling and first-piece checks may still require operator input.
How Do You Set Up Repeat Orders More Consistently?
Save the settings from an approved run. Record the job revision, board layout, material thickness, guide positions and folding settings that apply to the machine. If the controller stores job recipes, keep a separate record of any manual settings it cannot recall.
Use the saved setup as a starting point. If the board thickness, cover paper or layout changes, verify the new setup before releasing the job for production.
Does Changing Box Size Always Require a Full Setup?
No. The work depends on what changes in the open case layout. A length change may only require adjustments to the feed and guide positions on some models. A different spine width, board thickness or corner shape can also affect board positioning and folding. Group jobs that share board layouts or tooling where the production schedule allows.
How Do You Measure and Improve Changeover Time?
Record the total time from the last acceptable piece to the first approved piece. Break it down into material waiting, machine adjustment, trial runs and inspection. Compare similar job changes so that a simple size adjustment is not measured against a change that also requires different tooling.
Keep first-piece approval in the measurement. A shorter changeover should come from less waiting and fewer repeat adjustments. Track rejected trial pieces alongside elapsed time to see whether the new process improves both setup speed and consistency.